About Lobe pump
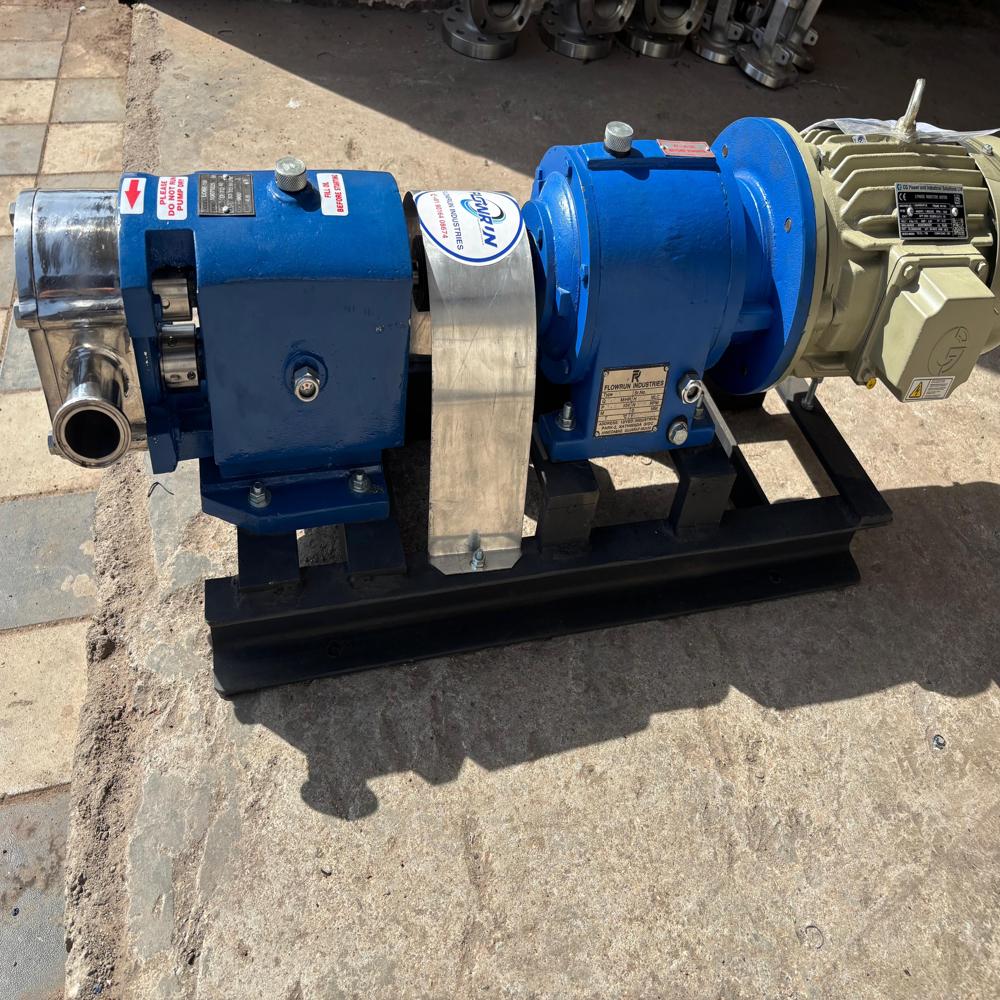
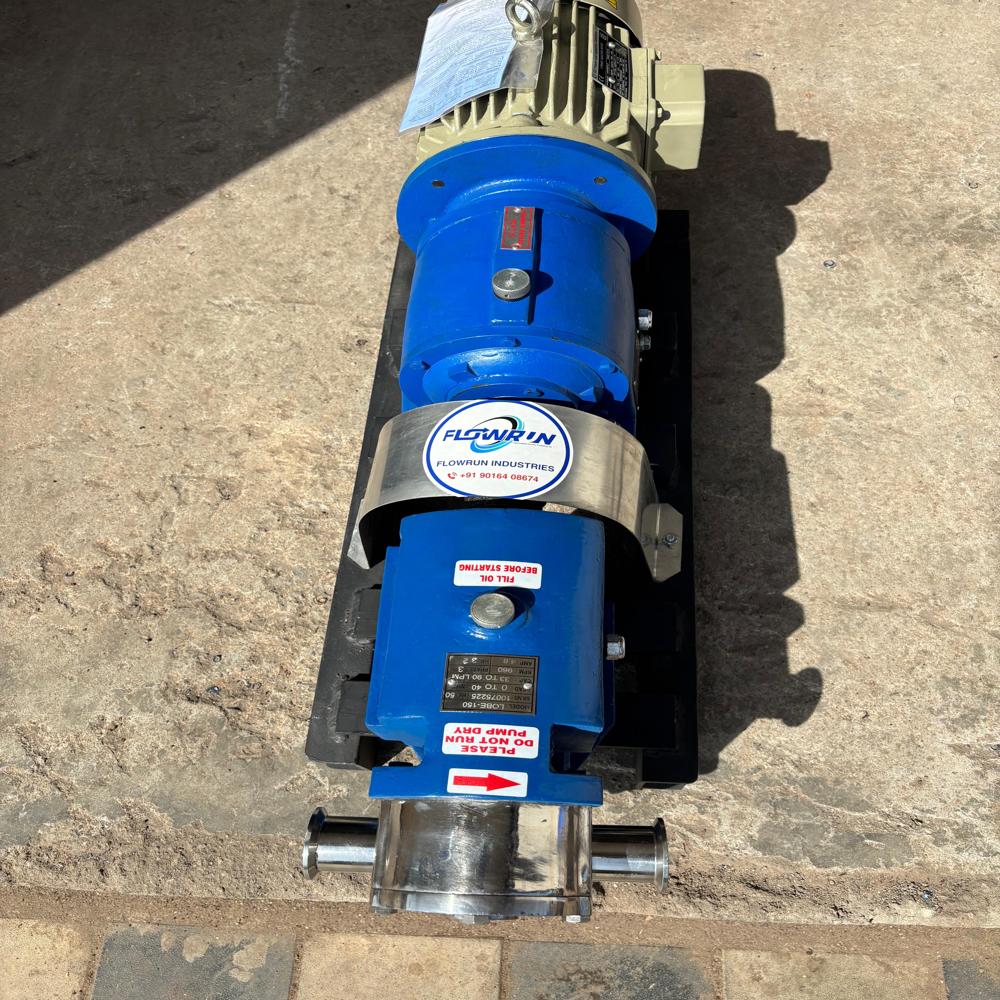
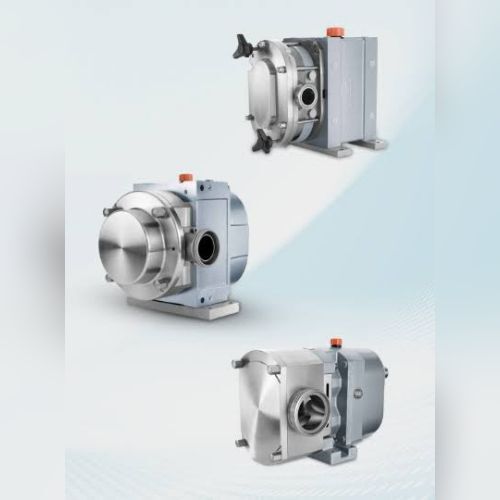
Rotary Lobe Pump is a heavy-duty positive displacement pump designed for efficient transfer of high-viscosity, abrasive, shear-sensitive, and solids-containing fluids. It is widely used in chemical, pharmaceutical, food processing, wastewater, sludge, slurry, and other industrial applications.
Gentle Handling of Sensitive ProductsThis lobe pump is specifically engineered for low-shear and gentle handling, making it the perfect choice for applications involving delicate or viscous food ingredients. Its rotary pump theory ensures minimal damage to product texture, preserving quality during transfer. The SS316 material offers corrosion resistance, helping maintain hygiene and durability in food settings.
Efficient Operation and Compact DesignThanks to its compact dimensions-15 inches in length, width, and height-the pump is suitable for installations with limited space. Priming is required, but its flooded suction type allows for efficient uptake and consistent flow, achieving a maximum suction of 100 mm. The robust mechanical seal prevents leaks, enhancing operational reliability.
Adaptability and High-Performance FeaturesSupporting a control system and operating at 50 Hertz, this lobe pump adapts to varying demands. It withstands discharge pressures of up to 5 kg/cm2, and is ideal for high-viscosity liquids, ensuring stable flow even in challenging conditions. The foot mounting type enables easy installation and maintenance, supporting both exporting and manufacturing supply chains across India.
FAQ's of Lobe pump:
Q: How does the lobe pump ensure gentle handling and low-shear transfer of food products?
A: The rotary theory of the lobe pump, combined with its innovative design, allows it to move products with minimal agitation. This reduces shear, preserving the texture and quality of sensitive food ingredients during transfer.
Q: What benefits does the SS316 material offer for this lobe pump in food applications?
A: SS316 stainless steel provides superior resistance to corrosion and contamination, making it highly suitable for food processing. It maintains hygiene standards and ensures a long service life, even under high temperature and pressure environments.
Q: When should priming be performed before operating this lobe pump?
A: Priming is required prior to operation to ensure the flooded suction type can effectively uptake liquids, preventing air pockets and ensuring smooth flow. This step is especially important when handling high-viscosity or delicate products.
Q: Where can this lobe pump be installed, considering its compact size?
A: With dimensions of 15 inches for length, width, and height, this pump is ideal for installations in areas with limited space. It can be easily mounted using the foot mounting type, making it flexible for various food processing setups.
Q: What is the process for maintaining the mechanical seals in this pump?
A: Regular inspection and cleaning are recommended for the mechanical seals to prevent leaks. It is advisable to follow maintenance guidelines provided by the manufacturer, ensuring consistent performance and reducing downtime.
Q: How does the control system support the pump's operations?
A: The integrated control system enables users to monitor and adjust pump speed (ranging from 250 to 1450 RPM) and flow rate. This adaptability enhances precision when handling diverse food products and viscosity levels.
Q: What are the main benefits of using this pump for high-viscosity liquids?
A: The pump's robust design, high discharge pressure (up to 5 kg/cm2), and flooded suction type allow it to efficiently handle high-viscosity liquids, preventing clogging and ensuring consistent product transfer with reliable performance.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
 Call Me Free
