About Chemical process pump
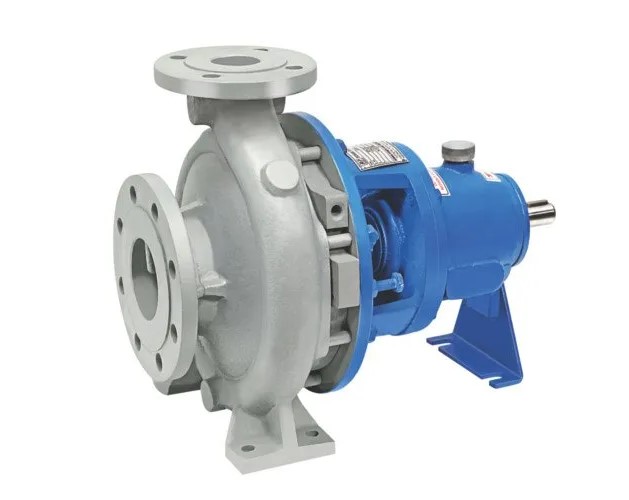
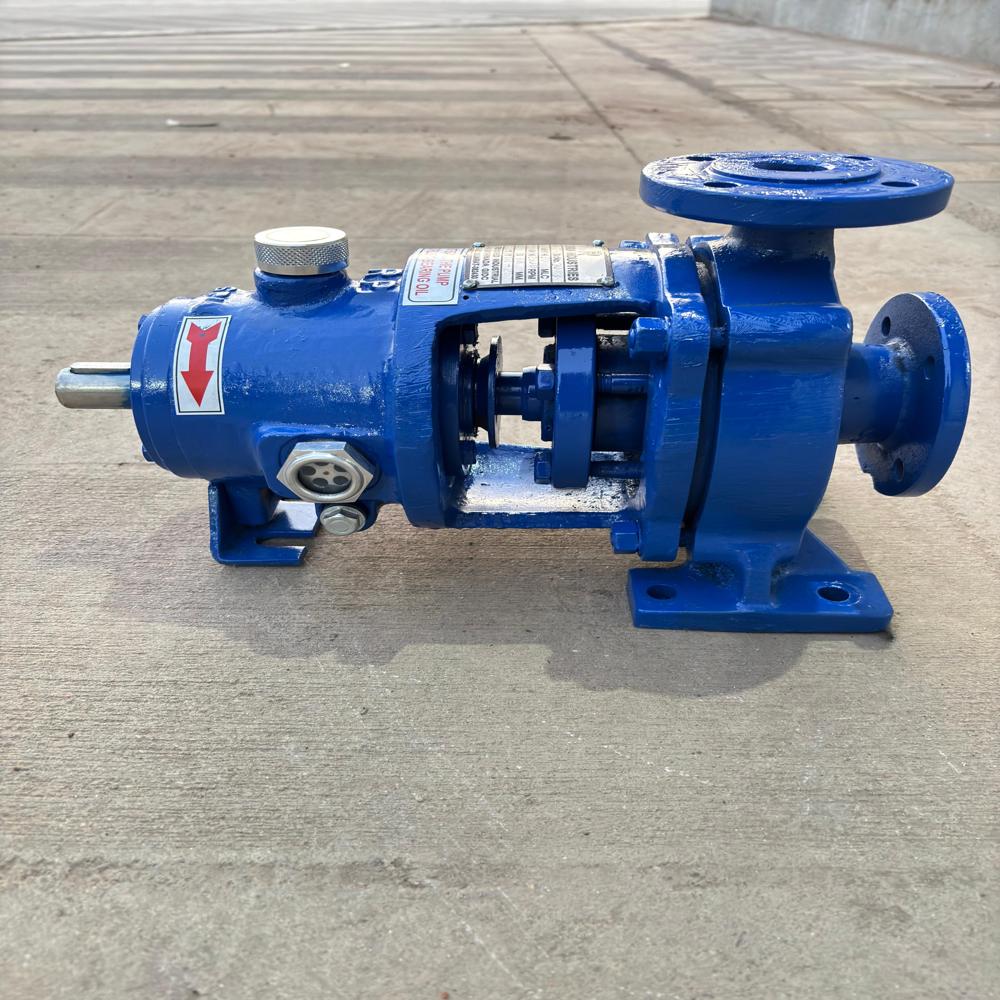
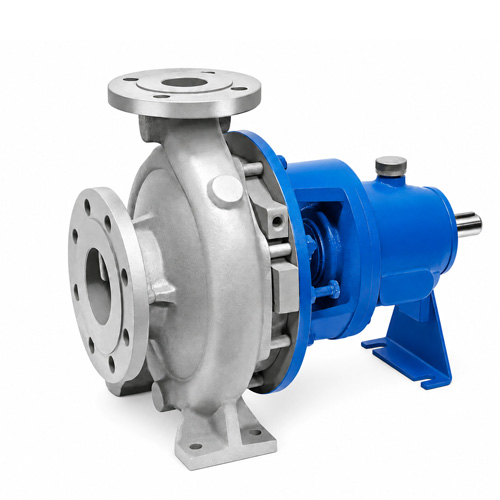
Discover the latest in fluid handling with our top-rated Chemical Process Pump, engineered for immaculate performance and extraordinary reliability. Featuring a choice of closed or semi-open impellers to suit your process requirements, this robust pump delivers excellent efficiency with its anti-friction ball bearings, replaceable stainless steel shaft sleeve, and chemical-resistant epoxy coating. Meeting international flange standards (ANSI/DIN/JIS) and supporting both manual and automatic controls, this versatile pump is designed for acids, alkalis, solvents, and slurries. Enjoy competitive pricing for equipment that combines industrial strength with easy maintenance and enduring corrosion resistance.
Versatile Applications for Diverse Industries
Our chemical process pump is tailored for a wide range of usage scenarios. It serves chemical plants, water treatment facilities, pharmaceutical manufacturing, and petrochemical operations. Designed to safely transfer acids, alkalis, solvents, and slurries, this pump is an essential asset for industries that demand reliable, heavy-duty liquid movement. Its robust construction ensures consistent performance, making it ideal for both routine operations and critical processes where safety and efficiency are paramount.
Certifications, Samples, and Supply Assurance
Certified to ISO 2858 and DIN 24256 standards, our chemical process pump meets stringent quality and safety benchmarks. Sample units can be provided for evaluation upon request, ensuring you assess the product's suitability prior to purchase. With a flexible exchange and sale price policy, we offer highly competitive pricing for bulk orders. Our supply ability accommodates both small and large-scale requirements, with prompt delivery and comprehensive customer support for every transaction.
FAQ's of Chemical process pump:
Q: How does the chemical process pump handle corrosive liquids safely?
A: The pump is constructed from corrosion-resistant materials such as stainless steel, Alloy 20, Hastelloy, and polypropylene, and is coated with a chemical-resistant epoxy. These features ensure long-lasting protection and performance when handling aggressive media like acids, alkalis, and solvents.
Q: What industries and applications are best suited for this chemical process pump?
A: This pump is ideal for use in chemical processing plants, water treatment systems, pharmaceutical manufacturing, petrochemical industries, and effluent transfer. Its ability to handle various corrosive liquids and slurries makes it a versatile solution for demanding industrial environments.
Q: When is it possible to request a sample or demonstration unit?
A: Samples or demonstration units are available on request. Please contact our sales team to discuss your requirements, and we will arrange for you to evaluate the pump's suitability for your process before finalizing your order.
Q: What control options are offered for this chemical process pump?
A: Depending on the model, control systems can be either manual or automatic. This versatility enables users to integrate the pump easily into existing systems and adapt operation to specific process needs.
Q: Where can the chemical process pump be installed?
A: Designed for industrial installation, the pump can be baseplate or flooded suction mounted. It supports horizontal end suction configurations, allowing flexibility in placement within your plant layout and ensuring easy maintenance access.
Q: How does having multiple impeller types benefit the process?
A: Offering both closed and semi-open impeller options allows users to select the most suitable type for their application. This flexibility helps enhance efficiency, manage different types of liquids or particulates, and extend the pump's operational life.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
