About Industrial centrifugal pump
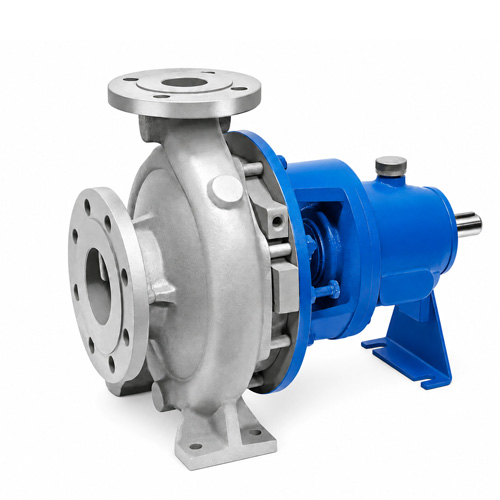
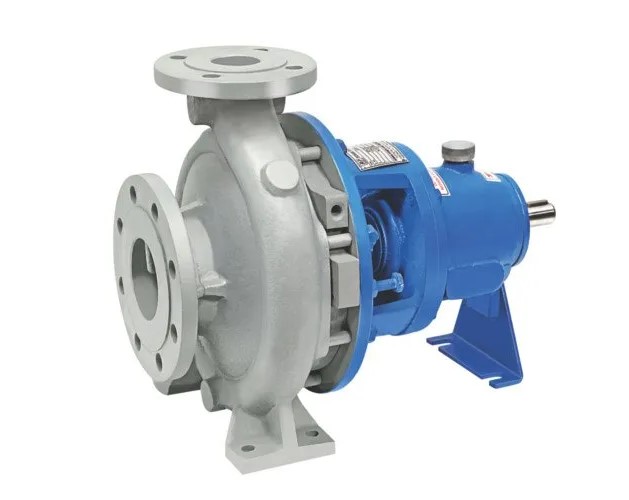
Procure the ultimate industrial centrifugal pump, engineered for fresh performance across diverse sectors. Featuring an enclosed impeller for lofty efficiency and a lustrous design, it boasts a long service life with wear-resistant components. The robust structure with heavy-duty ball bearings and a stainless or high carbon steel shaft ensures reliability. Air-cooled and IP55 rated, this pump supports high flow rates up to 2000 m3/h and heads up to 160 m. Suitable for water, oil, chemical processing, and more, it is the popular choice for those demanding premium quality, easy maintenance, and versatile customization.
Extensive Application Versatility & Competitive Edge
This industrial centrifugal pump is ideal for water supply, chemical processing, oil transfer, irrigation, and handling industrial fluids. Its adaptability suits both standard and demanding applications, processing particles up to 6 mm. With self-priming and non-self-priming options, it caters to various industries. Competitive advantages include exceptional durability, high efficiency, robust construction, and ease of maintenance, making it a popular solution among manufacturers, suppliers, and exporters for large-scale and specialized operations.
FOB Port, Certifications, and Sample Offers
Our centrifugal pump is available for shipment from major FOB ports and comes with comprehensive export documentation. Receive a prompt quotation and attractive offer tailored to your requirements. We provide sample availability for evaluation before bulk procurement. All products are certified to international standards such as ISO 2858/DIN 24255, ensuring quality and compliance. Count on hassle-free logistics, timely shipment, and certified performance for all your industrial needs.
FAQ's of Industrial centrifugal pump:
Q: How does the enclosed impeller enhance pump performance?
A: The enclosed or closed impeller design increases pumping efficiency and minimizes leakage, ensuring lustrous operation with improved energy savings and consistent fluid delivery.
Q: What are the main benefits of using heavy-duty ball bearings and wear-resistant components?
A: Heavy-duty ball bearings and wear-resistant components prolong the service life of the pump, reduce maintenance frequency, and provide reliable performance even in demanding industrial environments.
Q: When is it necessary to use self-priming versus non-self-priming models?
A: Self-priming models are ideal when the pump may need to handle intermittent suction or start-up flows, whereas non-self-priming pumps are suited for applications with a consistent fluid feed at the inlet.
Q: Where can this industrial centrifugal pump be installed for optimal results?
A: The pump is designed for horizontal installation and is suitable for water plants, chemical factories, oil refineries, irrigation fields, and various other industrial settings requiring robust, efficient fluid transfer.
Q: What is the process for customizing voltage, caliber, or control system options?
A: Customers can specify their desired voltages, caliber sizes, or control preferences during the quotation stage. The manufacturer then offers a custom solution tailored to these requirements before order confirmation.
Q: How does the pump ensure safe operation in harsh environments?
A: With an IP55 protection class, robust structure, and air-cooled system, the pump remains resilient against dust, water, and high temperatures, supporting ambient conditions up to 40C and providing maximum operator safety.




 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
 Call Me Free
